Custom Apparel Manufacturing Built on Engineering Precision & Trust
Learn about Bravane Industry's production infrastructure, ethical standards, leadership, and track record supplying global apparel brands.
Bravane Industry is a specialized OEM & ODM apparel manufacturer engineering custom streetwear, gymwear, sportswear, gymwear, and safetywear for international clothing labels, corporate enterprises, and athletic organizations.
We provide end-to-end production solutions—from sourced fabrics and digital pattern grading to computerized stitching, multi-technique printing/embroidery, and export packaging with strict quality control.
Manufacturing Standards & Sourcing Reliability
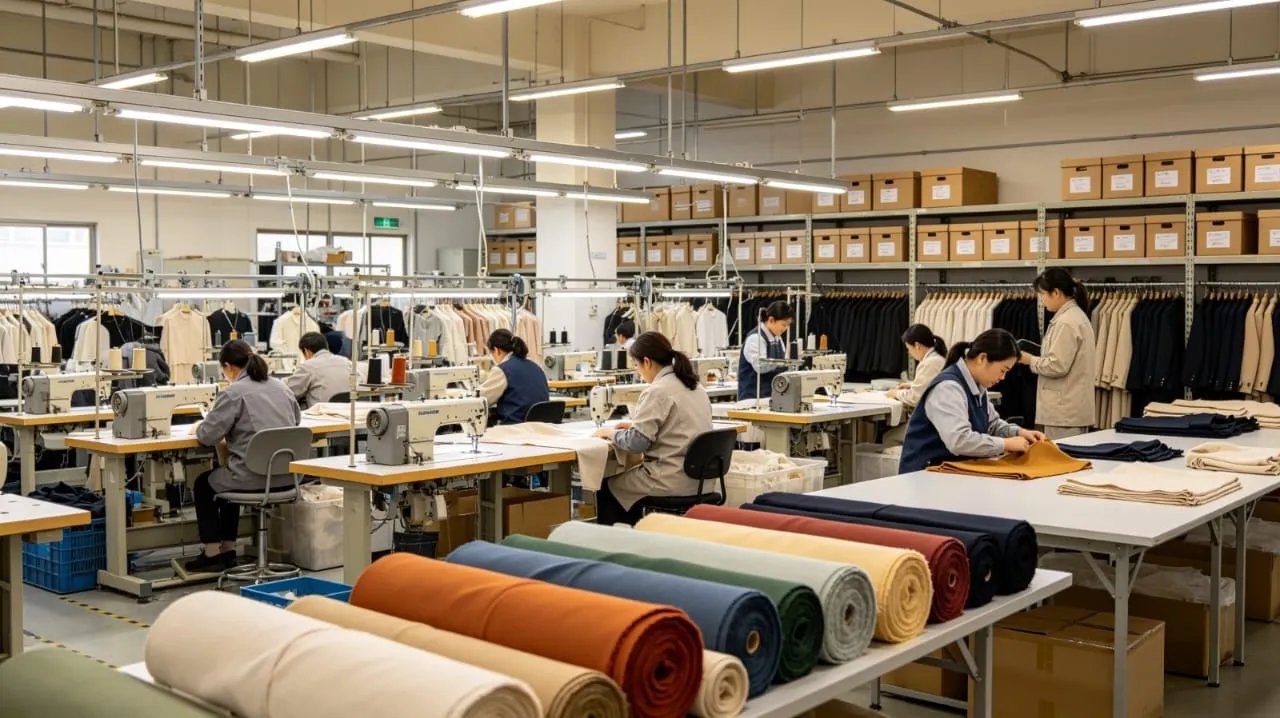 Bravane Industry Manufacturing Facility Floor
Built to Provide Transparent, Factory-Direct Apparel Manufacturing
Based in Sialkot, Pakistan—a globally renowned hub for textile craftsmanship and garment manufacturing—Bravane Industry brings specialized technical production expertise to international clothing brands, emerging streetwear labels, athletic organizations, and corporate buyers.
We operate with genuine business registrations, including Federal Board of Revenue (FBR) registration and active membership in the Sialkot Chamber of Commerce & Industry. Our manufacturing model bridges the gap between emerging brand founders seeking low-MOQ flexibility and established businesses requiring scalable OEM/ODM volume.
By keeping digital pattern development, fabric sourcing, cutting, stitching, printing, embroidery, and multi-stage quality control under direct factory oversight, we ensure transparent communication, honest material weights, and reliable international delivery.
Manufacturing Facilities & Departmental Capabilities
Our centralized manufacturing unit in Sialkot houses specialized production departments, providing complete end-to-end control from pattern drafting to export dispatch.
Pattern Engineering & Cutting
Digital Gerber/Lectra CAD pattern grading, automatic layer spreading, and laser precision cutting for zero grain distortion and exact grading across sizes XS–5XL.
- Automated fabric spreading tables
- Digital nesting for minimal waste
- Tolerance control: +/- 0.5 cm
Dedicated Stitching Lines
Specialized lines for heavy French terry, technical elastane gymwear, flatlock sportswear, and reinforced safety workwear.
- 4-thread & 5-thread overlock machinery
- 4-needle 6-thread flatlock seams
- Heavy-duty bar-tacking & twin-needle hem
In-House Printing & Dyeing
Complete decoration studio: automatic screen printing (puff, high-density, plastisol, water-based), direct-to-film (DTF), and all-over dye sublimation.
- Automatic screen printing presses
- High-density & silicone gel prints
- High wash durability & colorfastness
Computerized Embroidery
Multi-head computerized embroidery producing high-density 3D puff embroidery, flat crests, felt applique, and custom chenille patches.
- Up to 15 thread colors per design
- 3D foam puff & metallic threads
- Micro-detail precision stitch digitizing
Private Label & Custom Trims
Custom branded metal hardware, engraved aglets, woven damask neck labels, silicone badges, debossed leather patches, and custom drawcords.
- Woven & satin care labels
- Custom dyed zipper pulls & eyelets
- Barcode & SKU sticker integration
Packaging & Freight Forwarding
Individual frosted/polybag packing, custom retail boxes, moisture-barrier wrapping, carton drop-testing, and international shipping coordinated to agreed terms.
- Biodegradable & frosted ziplock bags
- Export-grade 5-ply double-wall cartons
- Air express (DHL/FedEx) & sea freight
Our Multi-Stage Quality Control Protocol
Quality is engineered into every stage of our workflow using international inspection parameters to ensure consistent, defect-free output.
Fabric & Raw Material Audit
Testing every fabric roll for exact GSM weight, yarn composition, 4-point visual flaws, and pre-shrinkage wash stability before cutting.
Pre-Production Sample Sign-Off
Constructing complete counter-samples for physical buyer fit, Pantone lab dip approval, and measurement calibration against tech pack specs.
Inline Workstation Inspection
Continuous roving QA inspections checking stitch tension, seam alignment, needle holes, and print placement during live assembly.
Post-Assembly & Finishing Check
100% garment inspection for loose thread trims, iron pressing, symmetrical dimensions, and correct private labeling placement.
Final Pre-Shipment Quality Audit
Randomized statistical sampling of sealed export cartons verifying packing accuracy, barcode scans, and carton integrity before export dispatch.
Ethical Standards & Environmental Commitments
We operate under transparent, verifiable social and environmental commitments designed to protect factory workers and client brand reputation.
Ethical Labor & Fair Wages
Strict adherence to zero-child-labor policies, fair wage compliance, regular regulated work shifts, clean dining areas, and workplace health and safety protections for floor operatives.
Skin-Safe & Eco-Friendly Materials
All cotton yarns, polyester blends, and textile dyes are procured from vetted mills adhering to non-toxic, skin-safe, and azo-free chemical guidelines safe for human skin and everyday athletic wear.
Standardized Quality Control Systems
Our standard operating procedures (SOPs), multi-point measurement checks, tension calibrations, and batch record archiving ensure rigorous quality consistency from raw fabric to final pack.
Fabric Scrap Recycling & Energy Efficiency
Fabric cutting remnants are systematically collected and sorted for textile recycling. In addition, our manufacturing floor uses energy-efficient servo-motor sewing machines and LED lighting throughout.
Experienced Technical Leadership
Our leadership team combines deep textile engineering expertise with international business management.
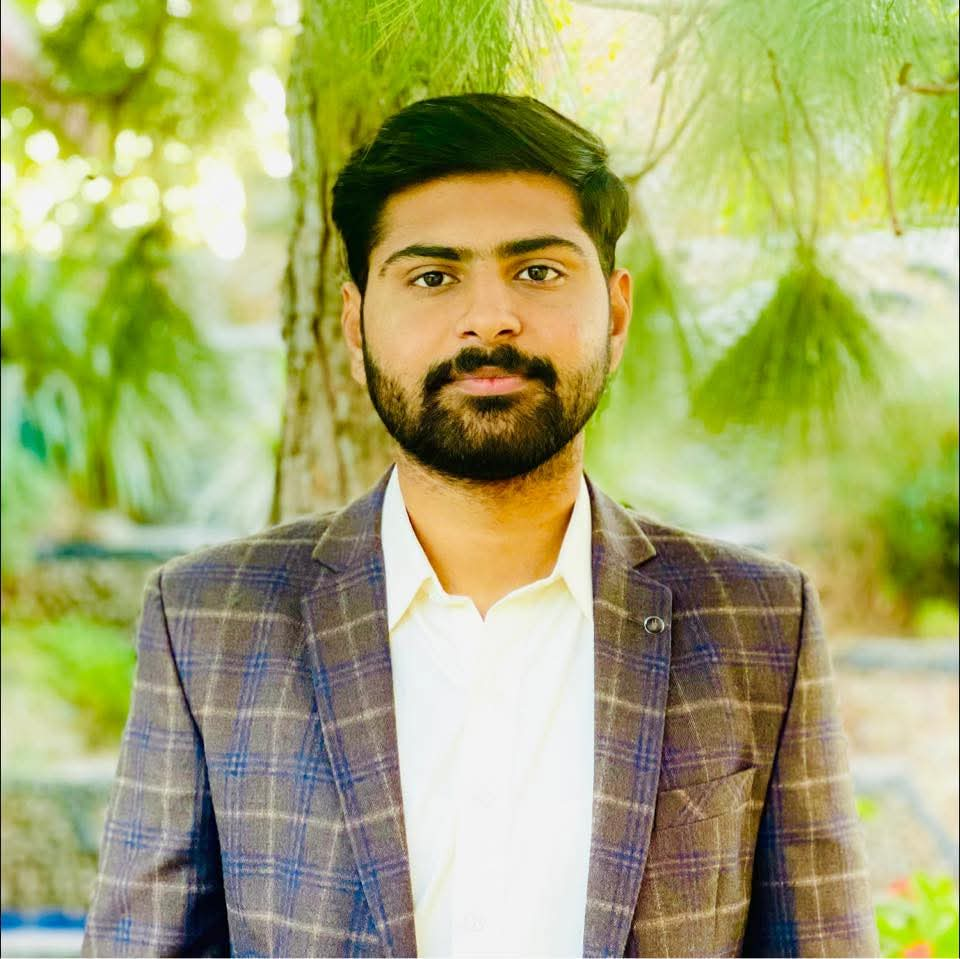
Araiz Maqsood
“Our mission is simple: to make custom apparel manufacturing transparent, technically accurate, and completely dependable for international brand builders.”
With an extensive background in textile manufacturing and export logistics, Araiz leads strategic operations, infrastructure modernization, and high-level client partnerships across North America, the UK, Europe, and Australia.
Contact CEO OfficeHead of Production & Engineering
Oversees in-house stitching lines, cutting schedules, and computerized pattern digitization. Specializes in technical sportswear construction, French terry knit engineering, and lean factory workflows.
- Specialized Industrial Engineering Experience
- Gerber/Lectra CAD Specialist
Senior QA & Compliance Manager
Directs the 5-stage QC protocol, raw material lab dips, fabric GSM calibration, and final pre-shipment statistical audits to maintain strict quality standards against critical defects.
- Quality Control & Audit Specialist
- Textile Physics & Testing Lead
Our Core Working Principles
What we stand for operationally—practical, buyer-focused commitments that protect your margins and schedule.
Low-MOQ Accessibility
We support emerging brands and capsule drops with flexible minimums starting from 25 pieces, enabling founders to test new concepts without holding risky excess inventory.
Milestone Transparency
No guessing games or disappearing representatives. We provide real-time photo and video milestones from sourced fabric through to final boxing and tracking numbers.
Strict Material Compliance
What is specified in your tech pack is exactly what goes into your garments. We never swap yarns, down-spec GSM weights, or alter agreed thread specifications.